The ISA-95 model explained, and where MES fits
The ISA-95 levels in plain English: what lives at each layer, how ERP, MES and automation talk to each other, and why the standard still matters.
ISA-95 Model
The ISA-95 model, also known as ANSI/ISA-95 or IEC 62264, is a global standard for enterprise and control system integration. The model is designed to provide a consistent framework for integrating business and manufacturing processes, enabling consistent information exchange between enterprise and control systems on the shopfloor.
ISA-95 is widely recognised and accepted as the de-facto standard for manufacturing system integration and is used by many companies around the world.
The model is developed and maintained by the International Society of Automation (ISA), a non-profit organisation that sets standards for industrial automation and control systems. Work on the standard began in the mid-1990s under ISA's SP95 committee, and Part 1 was first published in 2000. It has since grown to eight parts, and the core parts are adopted internationally as IEC 62264 (ISA). Its focus is mainly the boundary between Levels 3 and 4: the activities of manufacturing operations, and what ERP and MES/MOM exchange.
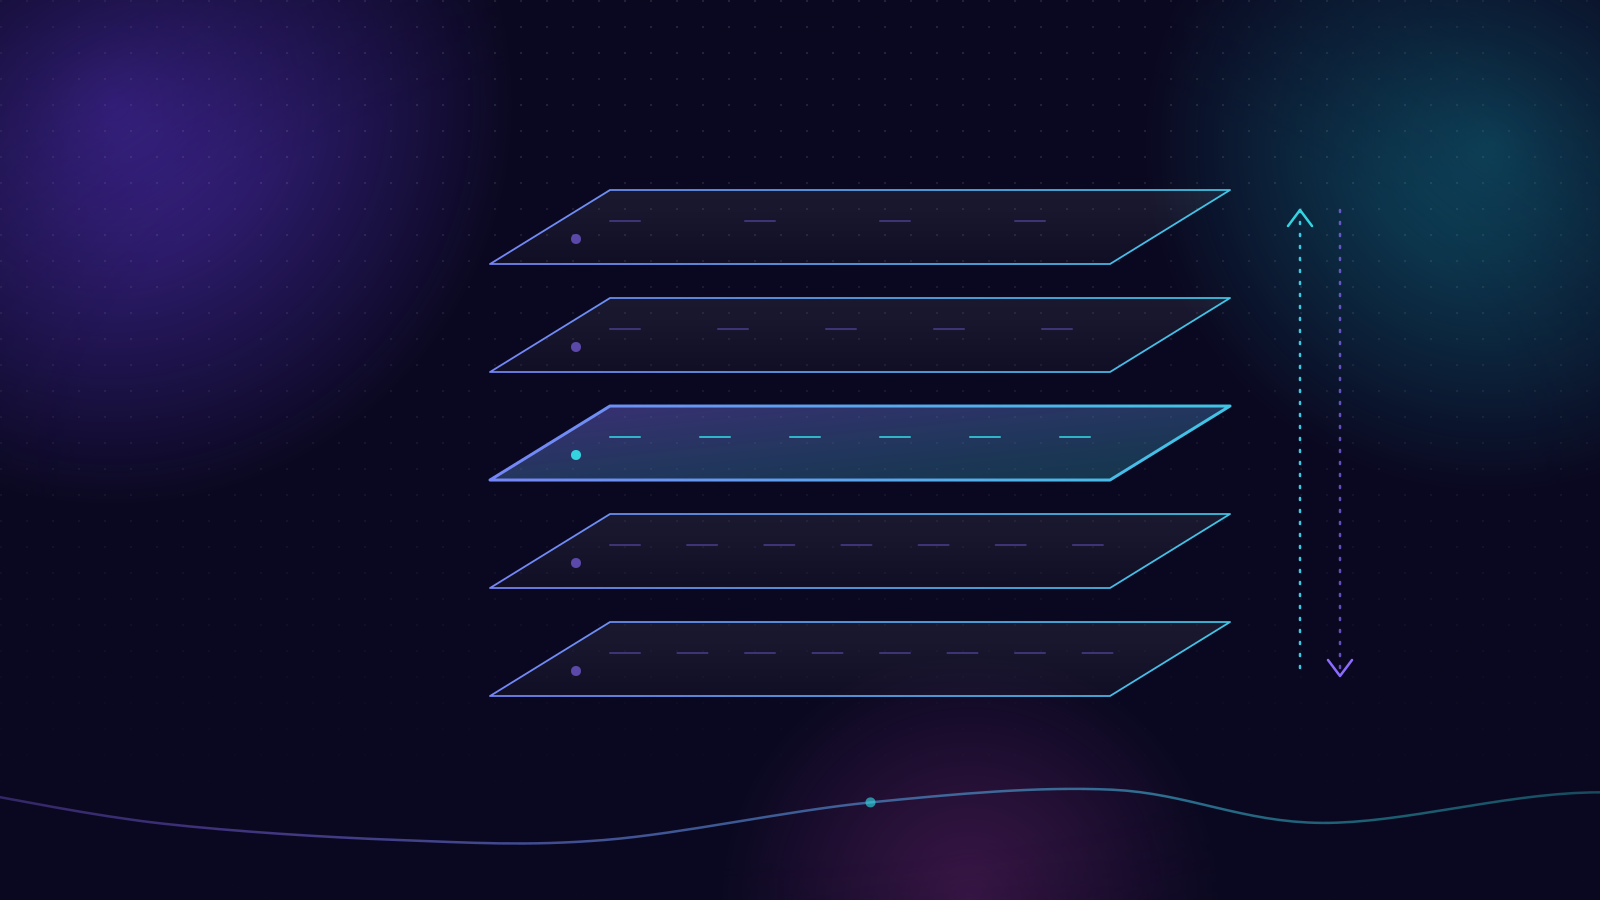
It consists of five levels, each representing a different layer of the manufacturing system. These levels are:
- Level 0 - The physical production process: the machines and equipment on the shopfloor.
- Level 1 - Sensing and manipulating the process: sensors, actuators, valves and other field devices, working in milliseconds.
- Level 2 - Monitoring and control: PLCs, DCS and usually SCADA, controlling and supervising the process in seconds.
- Level 3 - Manufacturing operations management: MES/MOM, working in shifts, hours, minutes and seconds.
- Level 4 - Business planning and logistics: ERP, working in months, weeks and days.
All of these layers communicate, allowing data to flow between the different systems in the factory.
This model is often depicted as a pyramid. For the purposes of MES we can consolidate levels 0, 1, and 2 together and consider them to be an output that MES can connect to in order to take real-time readings about the production process.
Communication between systems
Data flows from ERP to MES, information like the production order schedule and shared master data is sent to MES. MES then takes over and manages the factory operations, reporting key data back to ERP to keep the systems aligned. MES typically sends a subset of aggregated data back, it's not good practice to keep masses of detailed data in ERP, when MES is better suited to store, organise, and report on that information. ERP needs to know about anything related to costs, production volumes, order fulfilment, and inventory.
MES reads data directly from the OPC/PLC layer, typically through an OPC server. Other communication protocols such as MTConnect can also be used to collect data. PLCs not only read data about the process, but they can also control the process. MES can send instructions via OPC to control the process, such as starting/stopping production orders, or setting machine set points, removing the need for the operators to define the set points manually.
Deeper Dive into the ISA-95 layers
The physical equipment layer (Level 0) represents the manufacturing process, including the machines and other equipment in the production line. Physical sensors (Level 1) monitor the physical equipment layer, reading information about the process in real-time such as counts, machine stops, and process variables such as temperatures and speeds.
The monitoring and supervising layer (Level 2) includes the control systems that operate and monitor the physical equipment, typically implemented on programmable logic controllers (PLCs), which are small high-speed computers used to read sensor data and perform logic. PLCs are often programmed in "ladder logic", one of the IEC 61131-3 languages, which is coded graphically in a similar way to an electrical wiring diagram. This layer could involve distributed control systems (DCS), and supervisory control and data acquisition (SCADA) systems.
The manufacturing operations management layer (Level 3) includes the software systems that manage the manufacturing process, such as manufacturing execution systems (MES). If an MES isn't in place, then a collection of other applications could fill this space, such as:
- Quality Management Systems (QMS).
- Computerised Maintenance Management Systems (CMMS).
- Enterprise Asset Management (EAM) systems.
- Warehouse Management System (WMS).
Depending on the scope of the MES system, some of these applications may exist alongside an MES system. It's important to consider the full breadth of the MES system during the buying cycle, as some MES systems could lack some of this functionality. Even if you don't require the functionality up front, it's important to future-proof, so it's easier to expand the scope of the MES going forward.
This layer is responsible for coordinating the activities of the control layer to optimise the manufacturing process.
The business planning and logistics layer (Level 4) includes the software systems that manage the planning and logistics of the manufacturing process, such as:
- Enterprise Resource Planning (ERP) systems for finances, supply chain, and human resources.
- Supply Chain Management (SCM) systems.
- Customer relationship management systems.
This layer is responsible for coordinating the manufacturing process with the overall business objectives.
The ISA-95 model provides a standardised framework for integrating these different layers of the manufacturing system, enabling consistent information exchange between the different systems. This integration allows for real-time visibility into the manufacturing process, which can help to identify and resolve issues quickly, reduce downtime, and optimise the manufacturing process.
Vertical and horizontal
Two perspectives help make sense of how systems fit together.
Vertical is the ISA-95 stack itself. Data flows up from equipment, through PLCs and sensors, into MES/MOM and on to ERP. Instructions flow down. A temperature reading becomes a process parameter in MES/MOM, which becomes part of an OEE figure, which becomes a line in a monthly report.
Horizontal is the flow of work across departments and processes: a customer order moving from product design to planning, production, quality, warehousing and shipping. Each step may touch a different system.
Where IIoT and the unified namespace sit
IIoT lives in the connectivity layer, Levels 1 and 2. It's how data gets from equipment into the systems above. A unified namespace is an architecture for publishing that data, and MES/MOM's contextualised data, in one structured place. Neither replaces Level 3. More in IIoT doesn't replace MES and OPC UA, MQTT and UNS in plain English.
ISA-95 also defines the four areas of manufacturing operations management at Level 3: production, quality, inventory and maintenance. That's the scope of MOM, which I explain in MES vs MOM.
Benefits
One of the key benefits of the ISA-95 model is that it provides a standardised language for communication between different systems. This common language makes it easier for different systems to communicate with each other, reducing the risk of miscommunication and errors.
The model provides a standardised framework for data exchange. This framework makes it easier to exchange data between different systems, reducing the need for manual data entry and improving data accuracy.
Conclusion
The ISA-95 model is a widely recognised and accepted standard for integrating business and manufacturing processes. By providing a standardised framework for integrating different layers of the manufacturing system, the ISA-95 model gives everyone a common language for how information moves between systems. This integration can help to improve the efficiency and effectiveness of the manufacturing process, reducing downtime, and improving overall business performance.
Matt Barber
VP & General Manager for MES at Infor. Started as an MES developer, then ran projects, solution design and product. Writes about the smart factory, shopfloor AI and the MES/MOM foundations underneath them.